
Plan a textile stenter from fabric construction and the required drying, heat-setting or curing process. Specify edge holding, working width, overfeed and thermal conditions together, then verify dimensions and finished properties on representative material rather than compare chamber count alone. Run representative fabrics and approved finish chemistry at recorded entry moisture, overfeed and thermal conditions. Measure dimensions, residual moisture and the specified post-care or cured property, including center and edges. Demonstrate width change, restart and cleaning access, recording good finished length and actual process evidence rather than chamber setpoints alone. Submit the intended configuration and any OEM/ODM changes for project-specific feasibility review.
Plan a textile stenter from fabric construction and the required drying, heat-setting or curing process. Specify edge holding, working width, overfeed and thermal conditions together, then verify dimensions and finished properties on representative material rather than compare chamber count alone.
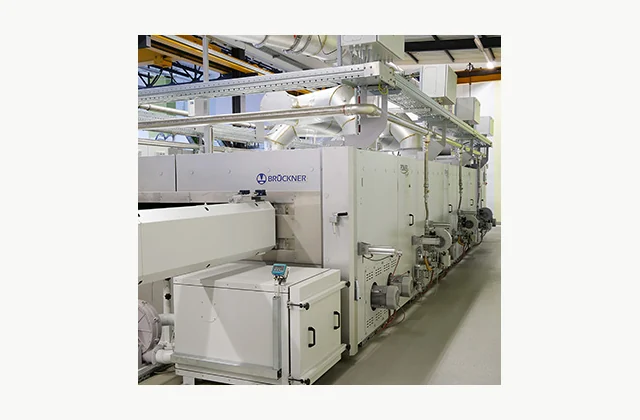
Shown as a configuration reference. Availability and the equipment offered for your project are confirmed separately.
Define the approved thermal process
Provide fiber blend, fabric construction, width, mass and whether the duty is drying, heat setting or chemical curing. Include material and coating thermal limits. A stenter can support different finishing routes, but the actual process window and supplied options must be established for the buyer's fabric rather than inferred from a family name.
Choose edge holding and width range
Specify pin or clip requirements, selvedge condition, entry spreading and minimum and maximum working widths. Review edge losses and any trimming scope. The machine's broadest chain setting does not guarantee secure handling of every curled, damaged or delicate edge without the correct entry devices and holding arrangement.
Control overfeed and fabric geometry
Define entry tension, overfeed, skew or bow correction and the desired exit dimensions. Identify correction modules actually included. A width setting alone cannot establish fabric geometry or residual shrinkage when longitudinal feed and upstream distortion are uncontrolled, particularly with elastic knits and dimensionally unstable constructions.
Verify zones airflow and actual exposure
Review heating source, zone control, airflow, exhaust and the method for measuring fabric temperature or moisture. Dwell depends on the active path and line speed. A controller setpoint or air temperature is not proof that the complete fabric has reached the required curing or heat-setting condition.
Coordinate entry chemistry and exit handling
Define upstream padding or coating, incoming moisture and the downstream cooling and winding route. Include chemical and exhaust responsibilities for the actual finish. A stenter quotation should distinguish its supplied modules from separate preparation or treatment systems, and the exit must preserve the dimensions achieved while the fabric cools.
Plan chain lint and heat-system service
Obtain chain, pin or clip maintenance instructions, lubrication requirements and access for cleaning filters and chambers. Qualified site specialists should assess lint and thermal hazards. Compare service work and energy on good finished fabric under the stated load, not merely a burner capacity or an unloaded machine demonstration.
Compare a complete textile stenter scope
| Decision | Information to compare |
|---|---|
| Define the approved thermal process | Fabric properties, dry/heat-set/cure duty and approved thermal process window |
| Choose edge holding and width range | Pin/clip choice, width range, selvedge condition, edge loss and entry devices |
| Control overfeed and fabric geometry | Tension/overfeed, bow/skew correction, width and longitudinal-dimension targets |
| Verify zones airflow and actual exposure | Heat source/zones, airflow/exhaust, fabric measurement and dwell calculation |
| Coordinate entry chemistry and exit handling | Incoming moisture/chemistry, preparation boundary, cooling and winding/tension interface |
| Plan chain lint and heat-system service | Chain/holding spares, lubrication, lint cleaning, service access and utility trial basis |
Plan installation and access
Qualified mechanical, thermal, electrical and site environmental specialists should coordinate foundations, heat supply, exhaust and the complete fabric route. Validate nip, chain and hot-zone protection and safe threading access. Retain utility and emission responsibilities, chain-service instructions and the measurement method used to confirm actual fabric exposure.
Agree acceptance evidence before ordering
Run representative fabrics and approved finish chemistry at recorded entry moisture, overfeed and thermal conditions. Measure dimensions, residual moisture and the specified post-care or cured property, including center and edges. Demonstrate width change, restart and cleaning access, recording good finished length and actual process evidence rather than chamber setpoints alone.
Define OEM/ODM engineering boundaries
OEM working widths, holding systems and approved thermal packages can be reviewed. ODM airflow, chain, curing or controls changes require engineering and fabric trials. Reference imagery establishes neither agency nor a guaranteed heat-setting, energy or emissions result for another construction, chemistry or site installation.
What should your textile stenter RFQ include?
- Fabric properties, dry/heat-set/cure duty and approved thermal process window
- Pin/clip choice, width range, selvedge condition, edge loss and entry devices
- Tension/overfeed, bow/skew correction, width and longitudinal-dimension targets
- Heat source/zones, airflow/exhaust, fabric measurement and dwell calculation
- Incoming moisture/chemistry, preparation boundary, cooling and winding/tension interface
- Chain/holding spares, lubrication, lint cleaning, service access and utility trial basis
- Destination, working environment, access and delivery constraints
- Installation responsibility, utilities and connection drawings
- Acceptance samples, documented test method, operator training and maintenance scope
- OEM/ODM changes requested: identification, tooling, interfaces or new design; engineering feasibility to be confirmed
Need OEM / ODM customization?
Submit branding, packaging, configuration or engineering requirements for this equipment. Include the target market, initial and annual quantities, required changes and acceptance criteria.
Customization feasibility, permitted branding, development responsibilities, minimum quantity, cost and lead time are reviewed for the proposed supplier and configuration before a quotation is confirmed.
Frequently asked questions
How do I define the approved thermal process?
Provide fiber blend, fabric construction, width, mass and whether the duty is drying, heat setting or chemical curing. Include material and coating thermal limits. A stenter can support different finishing routes, but the actual process window and supplied options must be established for the buyer's fabric rather than inferred from a family name.
How do I choose edge holding and width range?
Specify pin or clip requirements, selvedge condition, entry spreading and minimum and maximum working widths. Review edge losses and any trimming scope. The machine's broadest chain setting does not guarantee secure handling of every curled, damaged or delicate edge without the correct entry devices and holding arrangement.
How do I control overfeed and fabric geometry?
Define entry tension, overfeed, skew or bow correction and the desired exit dimensions. Identify correction modules actually included. A width setting alone cannot establish fabric geometry or residual shrinkage when longitudinal feed and upstream distortion are uncontrolled, particularly with elastic knits and dimensionally unstable constructions.
How do I verify zones airflow and actual exposure?
Review heating source, zone control, airflow, exhaust and the method for measuring fabric temperature or moisture. Dwell depends on the active path and line speed. A controller setpoint or air temperature is not proof that the complete fabric has reached the required curing or heat-setting condition.
How do I coordinate entry chemistry and exit handling?
Define upstream padding or coating, incoming moisture and the downstream cooling and winding route. Include chemical and exhaust responsibilities for the actual finish. A stenter quotation should distinguish its supplied modules from separate preparation or treatment systems, and the exit must preserve the dimensions achieved while the fabric cools.
How do I plan chain lint and heat-system service?
Obtain chain, pin or clip maintenance instructions, lubrication requirements and access for cleaning filters and chambers. Qualified site specialists should assess lint and thermal hazards. Compare service work and energy on good finished fabric under the stated load, not merely a burner capacity or an unloaded machine demonstration.
Reference information
- BRÜCKNER POWER-FRAME official product reference
- BRÜCKNER textile stenter official family or technical reference
Reference data and images explain equipment configurations. IndustryApex engineers confirm the offered model, specification and commercial scope in your project quotation.