
A closure inspection system checks agreed cap or closure features after application. Missing, tilted, damaged or incorrectly seated closures require suitable viewing geometry and a defined package-specific defect library. Visible closure inspection does not automatically establish opening torque or leak integrity; those need appropriate complementary tests. Challenge real missing, tilted and damaged closures across product positions and normal speeds; measure false rejects and confirm removal and fault response. OEM/ODM requests are assessed against the intended application, site interfaces and documented acceptance evidence; the reference photograph identifies a product family and does not confirm supply availability or an authorized brand relationship.
A closure inspection system checks agreed cap or closure features after application. Missing, tilted, damaged or incorrectly seated closures require suitable viewing geometry and a defined package-specific defect library.
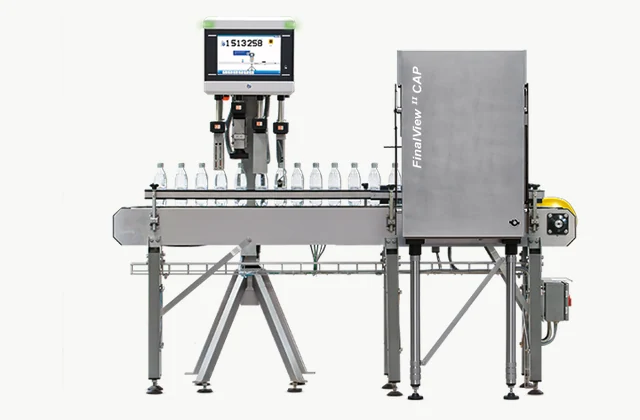
Shown as a configuration reference. Availability and the equipment offered for your project are confirmed separately.
What task does the cap and closure inspection system need to perform?
A closure inspection system checks agreed cap or closure features after application. Missing, tilted, damaged or incorrectly seated closures require suitable viewing geometry and a defined package-specific defect library.
Visible closure inspection does not automatically establish opening torque or leak integrity; those need appropriate complementary tests.
How should closure condition be specified?
Specify closure colors, tamper features, height, tilt and permitted appearance variation. A present cap can still be incorrectly seated or have a damaged band.
Separate a proven operating case from options that still require development. Supply representative samples or site information and ask the bidder to explain how the proposed design addresses the difficult conditions and the intended process interfaces.
Which configuration choices affect coverage and tracking?
Compare top and side views, lighting and product orientation. Associate each decision with the correct bottle and verify actual removal into the reject path.
| Decision | Evidence to compare | What the offer should clarify |
|---|---|---|
| Closure condition | Specify closure colors, tamper features, height, tilt and permitted appearance variation. A present cap can still be incorrectly seated or have a damaged band. | Included tools, input limits and the configuration needed for the stated duty. |
| Coverage and tracking | Compare top and side views, lighting and product orientation. Associate each decision with the correct bottle and verify actual removal into the reject path. | Supporting services, process interfaces and any excluded development work. |
| Application acceptance | Challenge real missing, tilted and damaged closures across product positions and normal speeds; measure false rejects and confirm removal and fault response. | Test method, inspection records, responsibility and treatment of deviations. |
What should be prepared before installation?
Provide stable conveyors, protected camera mounting, cleaning access and space for verified reject collection.
Include installation and service access in the quotation review. Confirm the working envelope and local connections against the real site, then agree the sequence for assembly, protective checks, training and first operation.
What evidence should establish application acceptance?
Challenge real missing, tilted and damaged closures across product positions and normal speeds; measure false rejects and confirm removal and fault response.
Document the conditions needed for repeatability, including preparation and operator actions. Agree how unresolved defects are handled and which site checks must be repeated before the buyer signs off the complete application.
How should service and repeatability be planned?
Inspect optics, mounting, trigger sensors and reject devices; control closure recipes and retained challenge samples.
Preserve setup, maintenance and verification records with the serial-number file. Training should cover safe cleaning, wear assessment and recovery, with responsibilities clear for any supporting equipment supplied by another party.
What can be customized through OEM or ODM?
Camera layouts, closure recipes and reject interfaces may be reviewed; new closure materials or shapes require validation.
Submit the requested changes with the cap and closure inspection system application, drawings and acceptance requirements. Distinguish standard options from new engineering and agree design ownership, validation, documentation and spare-part support before release. The illustrated manufacturer example is a technical reference; it does not establish stock, agency or permission to reproduce protected designs.
How should the quotation boundary be recorded?
Use the cap and closure inspection system inquiry to list base equipment, tooling, auxiliary services, commissioning and training separately. Record unresolved assumptions about closure condition and coverage and tracking before comparing prices. Keep the final configuration and accepted evidence together so later changes can be reviewed against a clear scope.
What should your cap and closure inspection system RFQ include?
- Cap and closure inspection system application and required finished result
- Closure condition: Specify closure colors, tamper features, height, tilt and permitted appearance variation. A present cap can still be incorrectly seated or have a damaged band.
- Coverage and tracking: Compare top and side views, lighting and product orientation. Associate each decision with the correct bottle and verify actual removal into the reject path.
- Representative input variation and difficult operating conditions
- Application risks and exclusions: Visible closure inspection does not automatically establish opening torque or leak integrity; those need appropriate complementary tests.
- Site and supporting services: Provide stable conveyors, protected camera mounting, cleaning access and space for verified reject collection.
- Acceptance method and retained evidence: Challenge real missing, tilted and damaged closures across product positions and normal speeds; measure false rejects and confirm removal and fault response.
- Maintenance and support scope: Inspect optics, mounting, trigger sensors and reject devices; control closure recipes and retained challenge samples.
- OEM/ODM changes requested: Camera layouts, closure recipes and reject interfaces may be reviewed; new closure materials or shapes require validation.
- Destination, local installation conditions and documentation language
- Drawings, samples, tooling ownership and revision control
- Operating sequence, changeovers, training and commissioning responsibilities
Need OEM / ODM customization?
Submit branding, packaging, configuration or engineering requirements for this equipment. Include the target market, initial and annual quantities, required changes and acceptance criteria.
Customization feasibility, permitted branding, development responsibilities, minimum quantity, cost and lead time are reviewed for the proposed supplier and configuration before a quotation is confirmed.
Frequently asked questions
What defines a suitable application for cap and closure inspection system?
A closure inspection system checks agreed cap or closure features after application. Missing, tilted, damaged or incorrectly seated closures require suitable viewing geometry and a defined package-specific defect library. Visible closure inspection does not automatically establish opening torque or leak integrity; those need appropriate complementary tests.
What should the buyer specify about closure condition?
Specify closure colors, tamper features, height, tilt and permitted appearance variation. A present cap can still be incorrectly seated or have a damaged band. Include representative variation and ask the bidder to identify restrictions before selecting the offered configuration.
How should coverage and tracking be compared?
Compare top and side views, lighting and product orientation. Associate each decision with the correct bottle and verify actual removal into the reject path. Confirm which tools, supporting services and operating conditions are included; require evidence for the actual application rather than an unloaded demonstration.
What acceptance test should be agreed for cap and closure inspection system?
Challenge real missing, tilted and damaged closures across product positions and normal speeds; measure false rejects and confirm removal and fault response. Agree the method, records and decision criteria before ordering, then retain the setup and results for repeatability checks after installation.
Which installation and service provisions need confirmation?
Provide stable conveyors, protected camera mounting, cleaning access and space for verified reject collection. Inspect optics, mounting, trigger sensors and reject devices; control closure recipes and retained challenge samples. Allocate local preparations and specialist service to named parties before delivery.
Can the cap and closure inspection system be customized through OEM or ODM?
Camera layouts, closure recipes and reject interfaces may be reviewed; new closure materials or shapes require validation. Submit the requested changes and drawings for feasibility review. New engineering requires agreed validation and documentation; the reference image does not establish a supply or brand relationship.
Reference information
- HEUFT FinalView II CAP - Closure inspection
- Product
Reference data and images explain equipment configurations. IndustryApex engineers confirm the offered model, specification and commercial scope in your project quotation.