
Blown film extrusion lines form a molten polymer tube, inflate and cool it, then collapse and wind the film. They differ from cast film lines that cool a flat web on rolls. Bubble stability, layer construction and winding requirements shape the useful configuration. Specify polymers, layer structure, layflat dimensions and film properties with intended converting or packaging use. Include recycled-feed controls and surface requirements. Film strength, sealing and optical behavior must be demonstrated on the proposed construction rather than inferred from layer count alone.
Blown film extrusion lines form a molten polymer tube, inflate and cool it, then collapse and wind the film. They differ from cast film lines that cool a flat web on rolls. Bubble stability, layer construction and winding requirements shape the useful configuration. Compare application fit, configuration and OEM/ODM scope through the buyer checklist below.
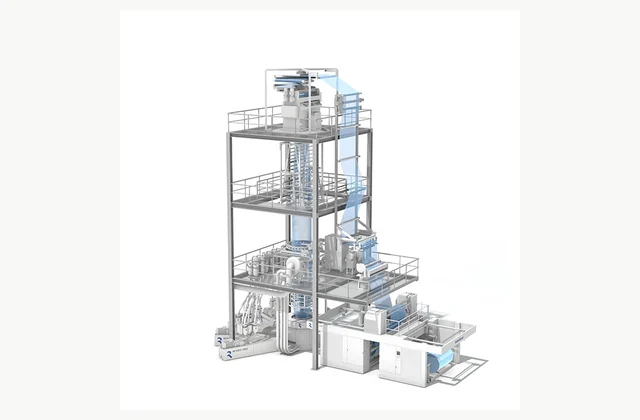
Shown as a configuration reference. Availability and the equipment offered for your project are confirmed separately.
Film construction: application and input specification
Blown film extrusion lines form a molten polymer tube, inflate and cool it, then collapse and wind the film. They differ from cast film lines that cool a flat web on rolls. Bubble stability, layer construction and winding requirements shape the useful configuration.
Specify polymers, layer structure, layflat dimensions and film properties with intended converting or packaging use. Include recycled-feed controls and surface requirements. Film strength, sealing and optical behavior must be demonstrated on the proposed construction rather than inferred from layer count alone.
Material compatibility needs a layer-by-layer review. A broad resin family description does not establish that every blend will process or bond as intended. Submit the actual formulation and define how future recycled-feed or additive substitutions are checked against accepted film performance.
Bubble system: configuration tradeoffs
Compare extruders, annular die, cooling, bubble control, haul-off and winding against the material and width range. Review tower height and the complete line balance. Additional layers or measurement options are meaningful only when they address a defined film function or quality requirement.
The bubble requires a suitable environment. Drafts, cooling conditions and building access can influence stability. Ask the supplier to state installation assumptions and test the normal operating range, avoiding a performance comparison that depends on an unusually favorable room condition.
| Decision | What to resolve | Useful evidence |
|---|---|---|
| Film construction | Material compatibility and layer purpose | Actual-formulation property tests |
| Bubble system | Cooling, stability and tower fit | Sustained defined-condition production |
| Roll delivery | Wrinkles, tension and converter behavior | Finished-roll conversion trial |
Process integration and handover points
Assign resin feeding, conditioning where needed, extrusion, bubble handling, treatment, slitting and roll delivery. Coordinate trim recovery and downstream printing or lamination. Define accepted roll dimensions and reject identification so startup or unstable film is separated from qualified product.
Gauge control is only useful with a defined measurement and acceptance method. Specify useful film width, sampling and the treatment of edge or trim regions. Compare accepted film across and along the roll rather than selecting a single favorable strip from the bubble.
Installation and maintainable operating arrangements
Review building height, platforms, cooling air, power and maintenance access with the complete tower. Include die service and reel handling routes, ambient conditions and the proposed air-management arrangement. A machine footprint without vertical access and utilities is incomplete for installation planning.
Collapsing and winding can introduce problems after extrusion. Wrinkles, blocking, tension variation and roll build matter to the converter. Review these stages with the intended thickness and surface, then run representative rolls through the next process where its behavior governs acceptance.
Acceptance evidence for roll delivery
Produce the intended film construction using specified materials and assess gauge distribution, appearance, mechanical or sealing properties and roll quality. Include startup and normal product changes. Test film after winding and relevant conditioning rather than judging a stable bubble visually.
Product changes need an actual procedure. Switching layers, color or formulation may create transition material and require cleaning or adjustment. Record the accepted-film recovery and waste from a meaningful change rather than treating recipe memory as proof of effortless flexibility.
OEM/ODM scope and future changes
ODM may include layer architecture, die and cooling arrangements, film treatment and winding interfaces. Agree material recipes, trial methods and tool ownership. OEM labels and manuals are separate from qualifying a new barrier, recycled or end-use film claim.
Keep the approved formulation, die, cooling and winding configuration with quality records. A changed packaging requirement may affect several stages at once. Review sealing, conversion and film-property evidence before presenting a revised multilayer construction as equivalent routine output.
Image reference: Reifenhauser EVO blown film line. The illustrated manufacturer configuration does not establish stock, an agency appointment or permission to relabel it. OEM/ODM requests require a written feasibility response for the actual proposed equipment.
Include these application details in your quotation request:
- Polymer formulations and layer architecture
- Layflat width, gauge and useful-film definition
- Mechanical, optical and sealing criteria
- Recycled-feed identity and control limits
- Extruder, die and bubble-cooling concept
- Tower height, platforms and ambient conditions
- Treatment, slitting and trim-return scope
- Winder, core and converter interfaces
- Actual-construction rolled-film acceptance
- OEM/ODM layer design and qualification ownership
What should your blown film extrusion line RFQ include?
- Polymer formulations and layer architecture
- Layflat width, gauge and useful-film definition
- Mechanical, optical and sealing criteria
- Recycled-feed identity and control limits
- Extruder, die and bubble-cooling concept
- Tower height, platforms and ambient conditions
- Treatment, slitting and trim-return scope
- Winder, core and converter interfaces
- Actual-construction rolled-film acceptance
- OEM/ODM layer design and qualification ownership
Need OEM / ODM customization?
Submit branding, packaging, configuration or engineering requirements for this equipment. Include the target market, initial and annual quantities, required changes and acceptance criteria.
Customization feasibility, permitted branding, development responsibilities, minimum quantity, cost and lead time are reviewed for the proposed supplier and configuration before a quotation is confirmed.
Frequently asked questions
What inputs determine selection of blown film extrusion line?
Specify polymers, layer structure, layflat dimensions and film properties with intended converting or packaging use. Include recycled-feed controls and surface requirements. Film strength, sealing and optical behavior must be demonstrated on the proposed construction rather than inferred from layer count alone.
How should I compare bubble system options?
Compare extruders, annular die, cooling, bubble control, haul-off and winding against the material and width range. Review tower height and the complete line balance. Additional layers or measurement options are meaningful only when they address a defined film function or quality requirement.
Which adjoining operations need to be specified?
Assign resin feeding, conditioning where needed, extrusion, bubble handling, treatment, slitting and roll delivery. Coordinate trim recovery and downstream printing or lamination. Define accepted roll dimensions and reject identification so startup or unstable film is separated from qualified product.
What is a useful acceptance trial for blown film extrusion line?
Produce the intended film construction using specified materials and assess gauge distribution, appearance, mechanical or sealing properties and roll quality. Include startup and normal product changes. Test film after winding and relevant conditioning rather than judging a stable bubble visually.
Which OEM/ODM changes can I request?
ODM may include layer architecture, die and cooling arrangements, film treatment and winding interfaces. Agree material recipes, trial methods and tool ownership. OEM labels and manuals are separate from qualifying a new barrier, recycled or end-use film claim.
What application boundary is easy to overlook?
Material compatibility needs a layer-by-layer review. A broad resin family description does not establish that every blend will process or bond as intended. Submit the actual formulation and define how future recycled-feed or additive substitutions are checked against accepted film performance.
Reference information
- Reifenhauser EVO blown film line official reference
- Reifenhauser related technology or portfolio reference
Reference data and images explain equipment configurations. IndustryApex engineers confirm the offered model, specification and commercial scope in your project quotation.