
METAL FABRICATION
CNC press brake
Specify the actual bend sequence before choosing tonnage, tooling and CNC axes.
Explore the buying guideReference: Durma AD-S series

Equipment category
Compare cutting, forming, machining and joining equipment around real workpieces, tolerances and accepted production output.
Specify the actual bend sequence before choosing tonnage, tooling and CNC axes.
Explore the buying guideReference: Durma AD-S series
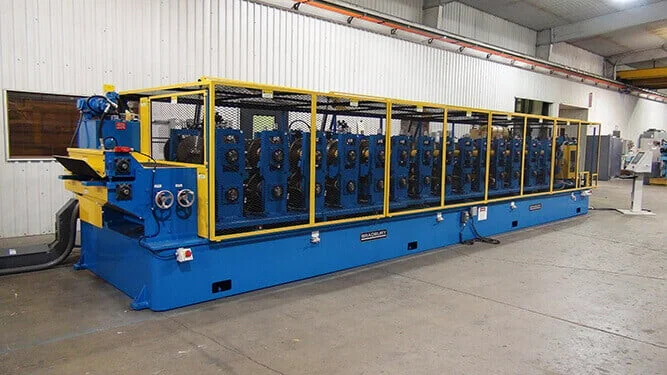
Specify finished profiles and coil properties before selecting a roll-forming line.
Explore the buying guideReference: The Bradbury Group QTR purlin roll forming line
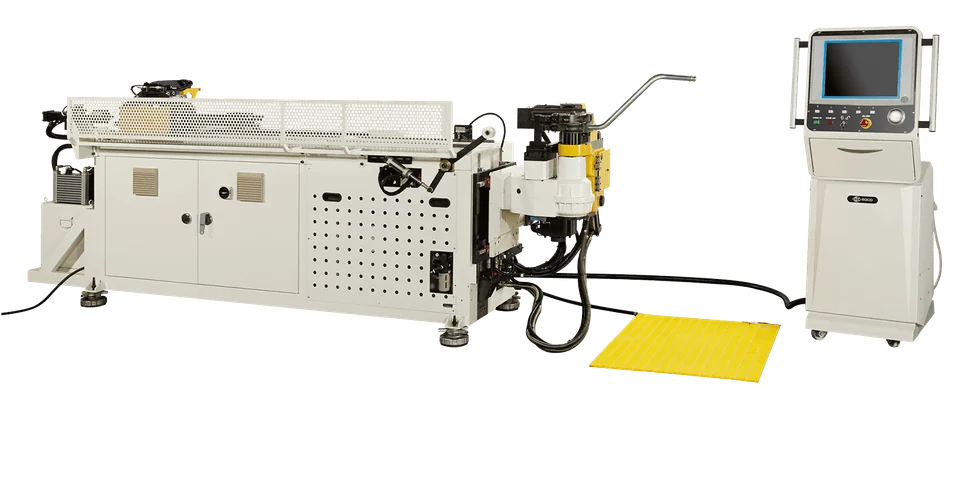
Select CNC tube bending from the complete tube drawing and tooling plan.
Explore the buying guideReference: SOCO Machinery A series (pictured SB-30X4A configuration)
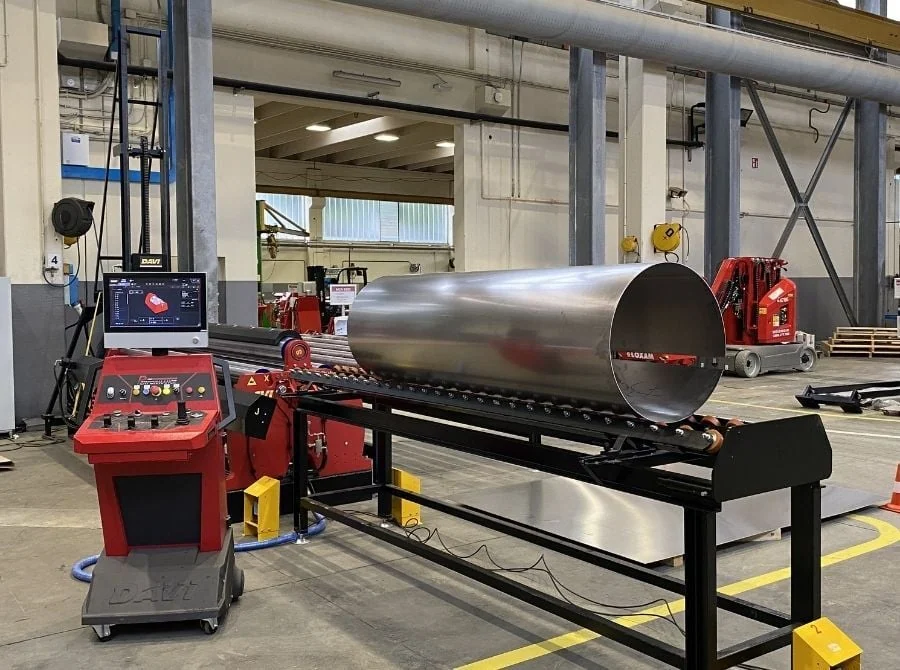
Specify cylinder geometry and plate grade before comparing rolling-machine capacity.
Explore the buying guideReference: DAVI MCA range

Compare CNC punching machines with the intended hole patterns, tools and formed features.
Explore the buying guideReference: JFY International MT300E
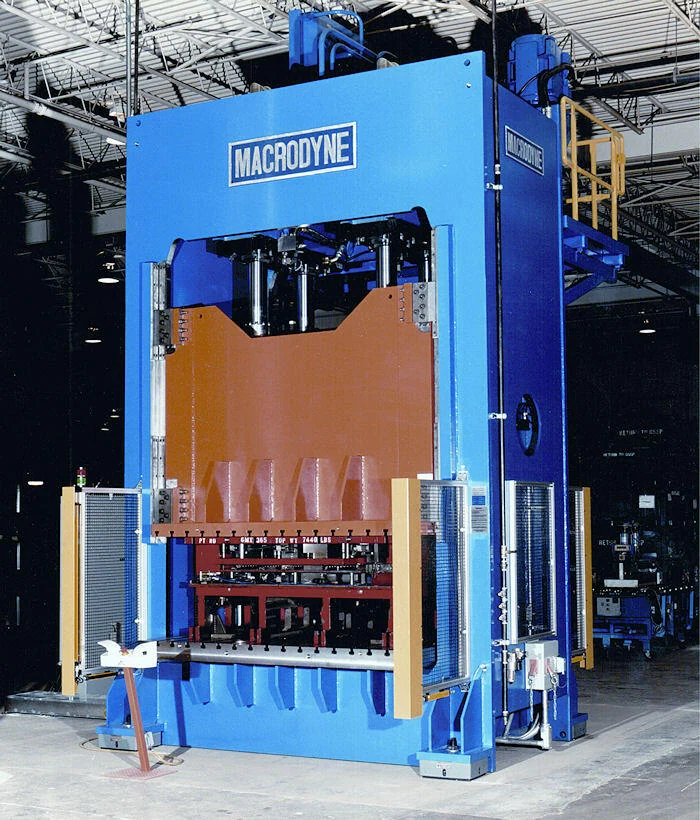
Specify the forming process and die before comparing hydraulic press tonnage.
Explore the buying guideReference: Macrodyne Metalforming hydraulic press family

Compare automatic panel bender proposals around panel geometry, bend sequence and automated blank handling. Define the process boundary, supporting equipment and acceptance evidence before choosing a configuration. Send the same application details to each bidder and include project-specific OEM or ODM requirements in the initial inquiry.
Explore the buying guideReference: Salvagnini P2 panel bender

Compare sheet metal folding machine proposals around fold geometry, beam-tool clearance and supported sheet positioning. Define the process boundary, supporting equipment and acceptance evidence before choosing a configuration. Send the same application details to each bidder and include project-specific OEM or ODM requirements in the initial inquiry.
Explore the buying guideReference: RAS FLEXI2bend

Compare angle and section bending roll proposals around profile orientation, section-specific rolls and accepted bend shape. Define the process boundary, supporting equipment and acceptance evidence before choosing a configuration. Send the same application details to each bidder and include project-specific OEM or ODM requirements in the initial inquiry.
Explore the buying guideReference: KNUTH KPB 81
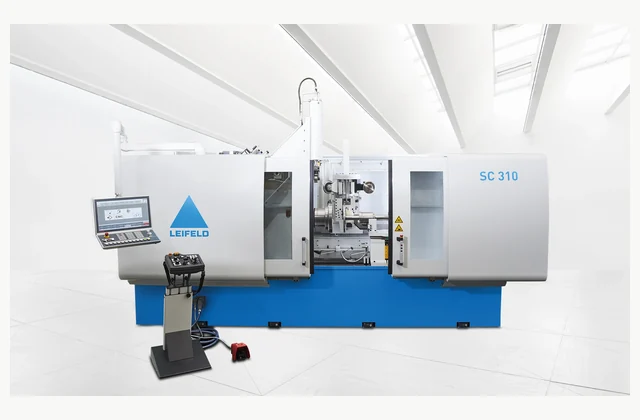
Compare cnc metal spinning machine proposals around rotational part geometry, material condition and controlled spinning paths. Define the process boundary, supporting equipment and acceptance evidence before choosing a configuration. Send the same application details to each bidder and include project-specific OEM or ODM requirements in the initial inquiry.
Explore the buying guideReference: LEIFELD SC 310 spinning center
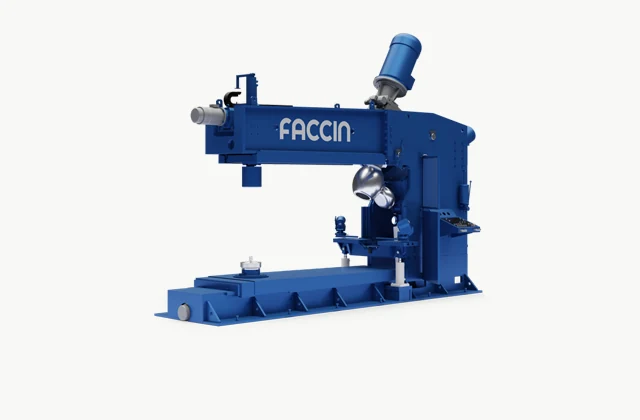
Compare plate dishing and flanging system proposals around dished-head geometry, forming sequence and plate-handling responsibility. Define the process boundary, supporting equipment and acceptance evidence before choosing a configuration. Send the same application details to each bidder and include project-specific OEM or ODM requirements in the initial inquiry.
Explore the buying guideReference: Faccin BF flanging machine (dished-head forming system reference)

Compare deep drawing press line proposals around draw geometry, material flow, tooling and automated transfer between forming stages. Define the process boundary, supporting equipment and acceptance evidence before choosing a configuration. Send the same application details to each bidder and include project-specific OEM or ODM requirements in the initial inquiry.
Explore the buying guideReference: AP&T Automated gutter production cell, deep-drawing application reference

Compare servo stamping press proposals around force and energy through the stroke, die compatibility and synchronized strip feeding. Define the process boundary, supporting equipment and acceptance evidence before choosing a configuration. Send the same application details to each bidder and include project-specific OEM or ODM requirements in the initial inquiry.
Explore the buying guideReference: Schuler MSP 400 servo press with feeding equipment

A flywheel stores energy and an eccentric mechanism drives the slide through a fixed motion. Stamping force, available working energy and permitted off-center loading are separate limits. Flywheel-driven stamping mechanism; RFQ must distinguish usable energy from nominal press force.
Explore the buying guideReference: AIDA NC1

An integrated coil line unwinds strip, corrects coil set and indexes material into a stamping die. It supplies the press and must be specified as upstream handling rather than another forming press. Prepares and feeds coil into a press; it is a dedicated upstream module rather than another press.
Explore the buying guideReference: Dimeco Press feeding line

A cut-to-length line converts coiled strip into flat sheets by coordinating uncoiling, leveling, measuring, shearing and stacking. It is a sheet-producing line, distinct from slitting coils longitudinally or feeding a stamping press. Uncoils and cuts sheets to length; compare flatness, stack handling and coil range.
Explore the buying guideReference: Bradbury Group Heavy-gauge cut-to-length line

A precision coil leveler bends strip through alternating rolls to correct curvature and reduce residual shape defects. This equipment is selected for strip preparation, rather than the general task of straightening an individual fabricated part. Corrects residual curvature before processing; material yield behavior drives leveling setup.
Explore the buying guideReference: Bradbury Group eDrive roller leveler

A clamped tube is reshaped at its end by axial tooling, with staged punches or dies producing expansions, reductions, flares and sealing features. This is distinct from bending the tube centerline. Expands or reduces tube ends; tooling follows the required joint and sealing geometry.
Explore the buying guideReference: Numalliance PHC

Tube hydroforming expands a sealed tube inside a closed die using internal fluid pressure, often with coordinated axial feeding. It forms the tube body rather than only producing a flare or connector at the end. Forms tubes against a die using internal fluid pressure; define part geometry and sealing strategy.
Explore the buying guideReference: Schuler Automatic tubular hydroforming system

A metal extrusion press forces a prepared billet through a die to create a continuous profile. The guide concerns metal billet extrusion and its thermal tooling system, rather than a polymer screw extruder. Produces profiles through an extrusion die; billet handling and die workflow are part of the scope.
Explore the buying guideReference: Presezzi Extrusion Metal billet extrusion press
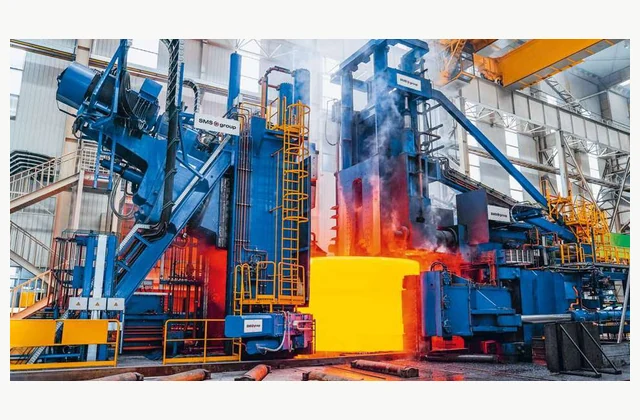
A ring rolling mill expands a pierced blank between driven rolls while reducing wall thickness; radial-axial arrangements also control ring height. It produces seamless rings, distinct from bending and welding strip into a ring. Expands seamless rings between rolls; ring section control defines its distinct process.
Explore the buying guideReference: SMS group Radial-axial ring rolling system
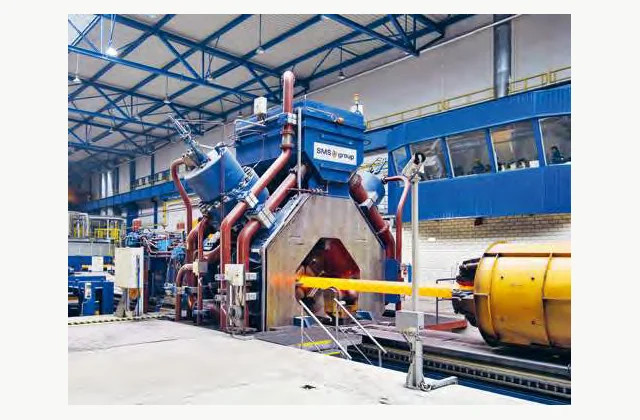
Radial forging applies repeated inward strokes from multiple tools around a rotating or advancing workpiece. Its buying boundary is controlled reduction of bars or hollow sections, beyond a general single-ram forging press. Uses radial tooling on bar or tubular workpieces; define core quality and axial feed strategy.
Explore the buying guideReference: SMS group SMX hydraulic radial forging machine

A screw drive converts rotational energy into a forging blow. Selection therefore considers available blow energy and the load developed as the die closes, rather than equating force alone with forging capability. Energy-controlled die forging with screw actuation; compare forming energy and die accommodation.
Explore the buying guideReference: LASCO SPP / SPR

Upsetting gathers material locally along a bar or shaft to create a larger section before subsequent shaping. Electric upsetters can heat the deformation zone while controlling axial feed and clamping. Redistributes bar ends for headed parts; blank length and gripping differ from sheet stamping.
Explore the buying guideReference: LASCO EH electric upsetter
Build a comparable request
Share the application, required output, destination, utilities, quantities and planned timing. For OEM / ODM projects, include the branding, configuration or engineering changes, sample approval and acceptance requirements.
Practical buying decisions
A comparable metal flow forming machine quotation starts with metal flow forming machine application and required process result, preform metallurgy and wall target, mandrel rollers and release. Record the required result, site interfaces and acceptance evidence in one revision-controlled RFQ. IndustryApex engineers use these inputs…
Read the guideA comparable rotary swaging machine quotation starts with rotary swaging machine application and required process result, starting stock and reduction sequence, internal geometry and axial feed. Record the required result, site interfaces and acceptance evidence in one revision-controlled RFQ. IndustryApex engineers use these inputs to…
Read the guideA comparable upset forging machine quotation starts with upset forging machine application and required process result, gathered volume and heated length, clamping and electrode condition. Record the required result, site interfaces and acceptance evidence in one revision-controlled RFQ. IndustryApex engineers use these inputs to define…
Read the guide
