
Cylindrical grinding finishes rotating external surfaces using a grinding wheel with work held between centers or in a chuck. Datums, slender-part support and thermal control determine whether the resulting shaft meets assembly requirements. Choose the configuration by shaft geometry and locating datums and plunge versus traverse grinding. Grind representative shafts and inspect diameter, taper, roundness, finish and datum runout after thermal stabilization. Include a wheel dress and a supported long-part trial. OEM/ODM requirements are reviewed against the intended process, site interfaces and acceptance evidence; the reference image identifies a product family and does not establish supply availability or an authorized brand relationship.
Cylindrical grinding finishes rotating external surfaces using a grinding wheel with work held between centers or in a chuck. Datums, slender-part support and thermal control determine whether the resulting shaft meets assembly requirements. Finishes external cylindrical surfaces; specify datum setup and accepted roundness.
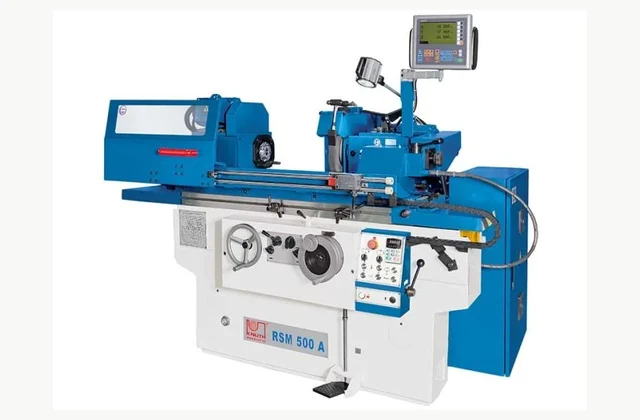
Shown as a configuration reference. Availability and the equipment offered for your project are confirmed separately.
What is the application scope for cylindrical grinding machine?
Cylindrical grinding finishes rotating external surfaces using a grinding wheel with work held between centers or in a chuck. Datums, slender-part support and thermal control determine whether the resulting shaft meets assembly requirements.
Finishes external cylindrical surfaces; specify datum setup and accepted roundness. Roundness alone does not establish alignment between separately ground journals or their functional datums.
How should shaft geometry and locating datums be specified?
Provide stepped diameters, lengths, shoulders, center holes, material hardness and allowances. Specify whether concentricity is measured to centers, a bore or an existing bearing journal.
The RFQ should make shaft geometry and locating datums a separate review item. Describe the expected variation, not only the easiest operating case, and ask the bidder to identify restrictions that affect the intended production mix.
What configuration evidence should be compared?
Compare wheel width, dressing, tailstock support and steady rests. Long slender shafts may deflect differently during grinding and inspection, so support conditions must be recorded.
Use a representative mix of routine work and the difficult cases that determine profitability. The offer should state the conditions under which each case is accepted, together with exclusions that would require further engineering or a new trial.
| Decision | Evidence to compare | Procurement consequence |
|---|---|---|
| Shaft geometry and locating datums | Provide stepped diameters, lengths, shoulders, center holes, material hardness and allowances. Specify whether concentricity is measured to centers, a bore or an existing bearing journal. | Defines the input and work envelope to be included in the offer. |
| Plunge versus traverse grinding | Compare wheel width, dressing, tailstock support and steady rests. Long slender shafts may deflect differently during grinding and inspection, so support conditions must be recorded. | Determines configuration, supporting equipment and exclusions. |
| Production acceptance | Grind representative shafts and inspect diameter, taper, roundness, finish and datum runout after thermal stabilization. Include a wheel dress and a supported long-part trial. | Establishes the agreed demonstration and inspection records. |
What must be prepared for installation?
Provide coolant filtration, grinding-mist extraction, leveling and room for shaft loading and measurement.
Resolve site interfaces early enough to affect the design. The commissioning plan should identify who supplies auxiliary services, who verifies protective functions and who signs off the first production setup.
How should production acceptance be demonstrated?
Grind representative shafts and inspect diameter, taper, roundness, finish and datum runout after thermal stabilization. Include a wheel dress and a supported long-part trial.
Use an agreed sampling method that covers the beginning, stable portion and end of the run. Document deviations and corrective actions before release; a video of motion cannot establish the required quality by itself.
Which service provisions protect repeatability?
Track wheel condition, dresser geometry, center wear, coolant temperature and workhead alignment against reference parts.
Preserve the approved configuration and commissioning records with the maintenance file. Confirm the service route for components supplied by other manufacturers so a fault does not leave the buyer coordinating unsupported interfaces.
What can be customized through OEM or ODM?
OEM probing and loading may be added; ODM slender or interrupted shafts require stiffness trials and a matching inspection fixture.
Submit the proposed changes with the cylindrical grinding machine duty and acceptance plan. Separate a purchased option from new engineering, and agree drawings, validation responsibility, documentation and spare-part support before design release. The manufacturer example is a technical reference only; customization does not imply permission to copy protected designs or use a brand.
Request an itemized offer that identifies tooling or auxiliaries, freight assumptions, commissioning, operator training and recurring consumables. Agree who supplies trial inputs and inspection instruments, and resolve deviations before comparing the complete project cost.
What should your cylindrical grinding machine RFQ include?
- Cylindrical grinding machine application and required process result
- Shaft geometry and locating datums: Provide stepped diameters, lengths, shoulders, center holes, material hardness and allowances. Specify whether concentricity is measured to centers, a bore or an existing bearing journal.
- Plunge versus traverse grinding: Compare wheel width, dressing, tailstock support and steady rests. Long slender shafts may deflect differently during grinding and inspection, so support conditions must be recorded.
- Representative input variation and difficult production cases
- Required acceptance evidence: Grind representative shafts and inspect diameter, taper, roundness, finish and datum runout after thermal stabilization. Include a wheel dress and a supported long-part trial.
- Site and utility scope: Provide coolant filtration, grinding-mist extraction, leveling and room for shaft loading and measurement.
- Service provision: Track wheel condition, dresser geometry, center wear, coolant temperature and workhead alignment against reference parts.
- OEM/ODM engineering scope: OEM probing and loading may be added; ODM slender or interrupted shafts require stiffness trials and a matching inspection fixture.
- Upstream preparation and downstream handling interfaces
- Destination country and applicable installation requirements
- Production schedule, changeover mix and operator availability
- Drawings, samples, inspection method and rejected-output criteria
Need OEM / ODM customization?
Submit branding, packaging, configuration or engineering requirements for this equipment. Include the target market, initial and annual quantities, required changes and acceptance criteria.
Customization feasibility, permitted branding, development responsibilities, minimum quantity, cost and lead time are reviewed for the proposed supplier and configuration before a quotation is confirmed.
Frequently asked questions
What defines the application boundary for cylindrical grinding machine?
Cylindrical grinding finishes rotating external surfaces using a grinding wheel with work held between centers or in a chuck. Datums, slender-part support and thermal control determine whether the resulting shaft meets assembly requirements. Finishes external cylindrical surfaces; specify datum setup and accepted roundness. Define the intended production result before comparing nominal ratings, and ask for evidence using the actual input conditions.
What should the cylindrical grinding machine RFQ state about shaft geometry and locating datums?
Provide stepped diameters, lengths, shoulders, center holes, material hardness and allowances. Specify whether concentricity is measured to centers, a bore or an existing bearing journal. Send the representative inputs and the difficult cases together, then require the supplier to state any restrictions or preparation steps needed to repeat the proposed result.
How should plunge versus traverse grinding be checked?
Compare wheel width, dressing, tailstock support and steady rests. Long slender shafts may deflect differently during grinding and inspection, so support conditions must be recorded. Ask the bidder to document the selected arrangement and exclusions against the real duty. Confirm which supporting components and setup work are included in the commercial scope.
What acceptance test is appropriate for cylindrical grinding machine?
Grind representative shafts and inspect diameter, taper, roundness, finish and datum runout after thermal stabilization. Include a wheel dress and a supported long-part trial. Agree the sampling method and rejection criteria before the trial, and keep configuration and inspection records for the later site-acceptance comparison.
What installation and service details should be confirmed?
Provide coolant filtration, grinding-mist extraction, leveling and room for shaft loading and measurement. Track wheel condition, dresser geometry, center wear, coolant temperature and workhead alignment against reference parts. Allocate local preparations and specialist support to named parties before shipment so commissioning and subsequent maintenance have a clear owner.
Can cylindrical grinding machine configurations be customized through OEM or ODM?
OEM probing and loading may be added; ODM slender or interrupted shafts require stiffness trials and a matching inspection fixture. Supply drawings and operating conditions for feasibility review. Engineering changes require agreed validation and documentation; a reference brand image does not establish an authorized supply or manufacturing relationship.
Reference information
- RSM 500 A - Conventional Cylindrical Grinder | KNUTH USA
- Conventional Grinding Machines | Surface & Cylindrical | KNUTH USA
Reference data and images explain equipment configurations. IndustryApex engineers confirm the offered model, specification and commercial scope in your project quotation.