
Holding small parts on a CNC router vacuum table requires zoned hold-down or gasketed spoilboard areas to maintain suction. Compare pump capacity, table configuration, part size limits and test retention with your nesting pattern and stock before ordering.
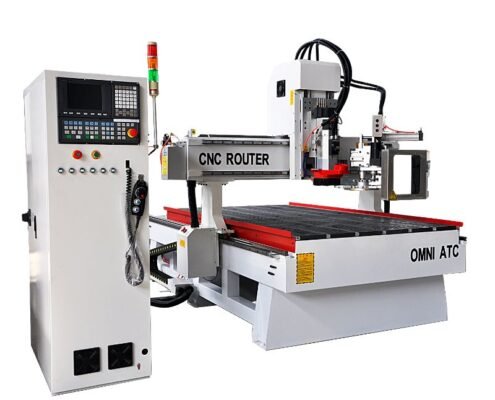
Shown as a configuration reference. Availability and the equipment offered for your project are confirmed separately.
Why small parts lose hold-down pressure
A full-size vacuum table loses suction when small parts cover only a fraction of the table area. Open table surface draws air around the part instead of through it, reducing clamping force. This becomes critical when the final profile cut separates a small part from the surrounding sheet, leaving minimal contact area at the moment cutting forces are highest.
Zoned vacuum and modular table arrangements
Zoned vacuum tables divide the work surface into independently controlled sections. Activate only the zones under your nested parts to concentrate airflow and maintain pressure. Modular vacuum tables use removable grid sections or individual pods, each with its own seal and connection. These configurations reduce wasted suction on empty table areas.
Request a dimensioned table drawing showing zone boundaries, valve locations and connection points. Confirm that the control system can activate zones independently and that the pump capacity supports the number of active zones in your typical nesting layout.
Spoilboard gasketing for irregular nesting patterns
Add a replaceable spoilboard with routed channels and foam or rubber gaskets to isolate suction around your parts. The gasket creates a seal between the part perimeter and the table surface, forming a closed chamber that maintains vacuum even when the surrounding table is open. This approach works for varying part shapes and sizes without reconfiguring the table hardware.
Test gasket compression and seal integrity with your thinnest stock and smallest retained part dimensions. Worn or improperly compressed gaskets leak air and reduce hold-down force. Include gasket material specification, replacement interval and spare gasket supply in the equipment quotation.
Pump capacity and achievable vacuum level
Pump capacity must overcome leakage around parts, through porous materials and across open table areas. Higher vacuum levels increase clamping force, but pump size, power consumption and noise increase accordingly. Oil-lubricated rotary vane pumps reach lower absolute pressures than dry pumps but require maintenance and oil disposal. Ring blowers and regenerative blowers provide continuous airflow at moderate vacuum levels with lower maintenance.
The Blue Elephant reference lists water circulation, ring blower, and rotary vane oil-free vacuum pump options from Taiwan and European suppliers [S1]. Request pump specifications with flow rate, ultimate vacuum, power consumption and connection requirements for the agreed table configuration and material type.
Material porosity and air leakage
Porous materials like MDF, particleboard and some softwoods allow air to pass through the workpiece, reducing effective vacuum. Seal the top surface with masking or use higher pump capacity to compensate for leakage. Non-porous materials like acrylic, solid hardwoods and laminates hold vacuum more effectively with lower pump demand.
Test hold-down with production stock rather than assuming nominal pump specifications translate to adequate clamping. Measure vacuum level at the part surface with a gauge during cutting to confirm that pressure remains sufficient through the complete tool path.
Part size, thickness and retention limits
Smaller parts have less surface area for vacuum to act on, and thinner parts deflect more easily under cutting forces. Define the minimum part width, length and thickness in your request. Ask the supplier to demonstrate hold-down with parts at those limits using the offered table, pump and spoilboard arrangement.
The final profiling pass that separates a part from the sheet creates the highest risk of movement or liftoff. Verify retention at that stage rather than relying on initial clamping during earlier operations. Adjust cutting depth, tool engagement or add mechanical clamps or pins for parts that cannot be held by vacuum alone.
Dust extraction interaction with vacuum hold-down
The NIOSH router dust-control study describes a jet and exhaust system that captured airborne dust at the cutting zone [S2]. Extractionhoods and hoses near the work surface can interfere with vacuum hold-down airflow or create turbulence that disrupts small part retention. Coordinate extraction hood placement, airflow direction and table vacuum arrangement in the equipment design.
Request a combined dust extraction and vacuum hold-down drawing showing hood position, duct routing and air balance. Confirm that the extraction system does not draw air from the vacuum table surface or reduce clamping pressure during cutting.
Buyer input worksheet: vacuum hold-down specification
| Input requirement | Your project data | Evidence to request |
|---|---|---|
| Smallest part width × length | [describe dimensions] | Demonstrated retention test with sample part |
| Thinnest material thickness | [describe thickness] | Clamping test through final profile cut |
| Material type and porosity | [material grade] | Pump capacity recommendation for material |
| Typical nesting density | [describe table coverage] | Zone configuration and active area calculation |
| Number of small parts per sheet | [count] | Spoilboard gasket layout for nesting pattern |
| Cutting forces and tool engagement | [tool diameter, feed, depth] | Hold-down force calculation and safety margin |
| Table area requiring vacuum | [describe area] | Pump flow rate and vacuum level at part surface |
Alternative hold-down methods and hybrid arrangements
Mechanical clamps, toggle clamps, edge stops and sacrificial tabs provide positive retention independent of vacuum. Use them for parts below the vacuum size limit, at sheet edges where vacuum sealing is difficult, or as backup when vacuum is lost. Vacuum-assisted mechanical clamping combines both methods, using vacuum to hold the sheet flat and clamps to secure small or critical parts.
Compare setup time, interference with tool paths and flexibility across different part geometries when choosing between pure vacuum, mechanical or hybrid hold-down. Include clamp hardware, installation points and adjustment procedures in the equipment specification.
Acceptance test for small-part vacuum hold-down
Run a complete nesting job with your smallest and thinnest production parts. Use the actual material grade, spoilboard configuration, pump and table arrangement included in the quotation. Measure vacuum level at the part surface during cutting and inspect parts for movement, chatter marks or incomplete cuts that indicate insufficient clamping.
Record setup time, gasket condition after the run and any parts that required manual intervention. Confirm that the tested configuration matches the delivered system specification and that replacement gaskets, spare vacuum fittings and maintenance procedures are documented in the equipment package.
Discuss your small-part hold-down requirements with IndustryApex engineers and request a complete vacuum table configuration andATC CNC router equipment solution for your nesting jobs.
Define your equipment requirements
Review the ATC CNC router buying guide for the complete equipment scope.
Discuss this equipment project ↗ · OEM requirements · ODM requirements. Configuration and feasibility are reviewed for your application.
Frequently asked questions
What table configuration holds small wood parts most reliably on a CNC router?
Zoned vacuum tables or spoilboard gasketing isolate suction around parts, maintaining clamping force when only a fraction of the table is covered. Test retention with your smallest part size, thinnest stock and actual nesting pattern before ordering.
How do I determine the required vacuum pump capacity for small parts?
Pump capacity depends on active table area, material porosity, part size and acceptable leakage. Request pump flow rate, ultimate vacuum level and power requirements for your material type and nesting density. Measure vacuum at the part surface during a trial cut to confirm adequate pressure.
Can porous materials like MDF be held securely with vacuum alone?
Porous materials allow air leakage through the workpiece, reducing effective vacuum. Seal the top surface, use higher pump capacity or add mechanical clamps for parts below the vacuum size limit. Test hold-down with production stock rather than assuming pump specifications guarantee retention.
What evidence should I request to verify small-part hold-down performance?
Request a demonstrated retention test using your smallest part dimensions, thinnest material and typical nesting layout. Ask for measured vacuum levels at the part surface, zone configuration drawings, gasket specifications and the complete pump and table arrangement included in the offer.
How does dust extraction affect vacuum table clamping force?
Extraction hoods near the work surface can draw air from the vacuum table or create turbulence that reduces clamping. Request a combined extraction and hold-down drawing showing hood placement, duct routing and air balance. Confirm that extraction does not interfere with part retention during cutting.
When should I use mechanical clamps instead of vacuum for small parts?
Use mechanical clamps for parts below the vacuum size limit, at sheet edges where sealing is difficult, or as backup when vacuum fails. Compare setup time, tool-path interference and flexibility across part geometries. Include clamp hardware and installation points in the equipment specification.
Reference information
- 1325 Linear ATC CNC Router | Automatic Tool Change CNC Machine | Blue Elephant
- NIOSH Hazard Controls HC6 – Control of Wood Dust from Automated Routers
Reference data and images explain equipment configurations. IndustryApex engineers confirm the offered model, specification and commercial scope in your project quotation.