
A flattening line rolls round wire into a controlled flat or profiled section. Reduction schedule, edge behavior and tension control determine the final strip rather than width alone. Choose the configuration by wire and final section and roll stands and tension. Roll representative wire and inspect section dimensions, edge integrity, straightness, surface and material properties where required. Include speed changes and coil transitions. OEM/ODM requirements are reviewed against the intended process, site interfaces and acceptance evidence; the reference image identifies a product family and does not establish supply availability or an authorized brand relationship.
A flattening line rolls round wire into a controlled flat or profiled section. Reduction schedule, edge behavior and tension control determine the final strip rather than width alone. Transforms wire into controlled flat profiles; roll setup and section tolerance define the process.
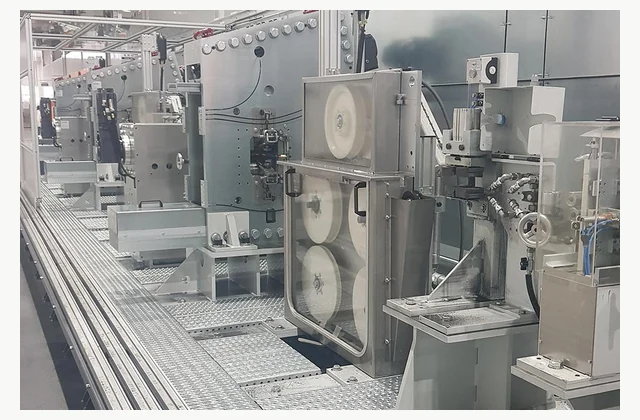
Shown as a configuration reference. Availability and the equipment offered for your project are confirmed separately.
What is the application scope for wire flattening rolling line?
A flattening line rolls round wire into a controlled flat or profiled section. Reduction schedule, edge behavior and tension control determine the final strip rather than width alone.
Transforms wire into controlled flat profiles; roll setup and section tolerance define the process. The same inlet diameter can yield different edge condition and properties when material temper or reduction sequence changes.
How should wire and final section be specified?
Provide alloy, inlet diameter, hardness, target width, thickness, edge profile and allowable camber. Include surface quality and any intermediate annealing requirements.
The RFQ should make wire and final section a separate review item. Describe the expected variation, not only the easiest operating case, and ask the bidder to identify restrictions that affect the intended production mix.
What configuration evidence should be compared?
Compare stand sequence, roll support, gap control, guides and take-up. Uneven reduction or tension can create thickness variation, edge cracks or twisting.
Build the comparison around the real component or duty. Identify which preparation steps happen elsewhere and which are supplied with the equipment; this prevents a successful isolated demonstration from being mistaken for a complete production solution.
| Decision | Evidence to compare | Procurement consequence |
|---|---|---|
| Wire and final section | Provide alloy, inlet diameter, hardness, target width, thickness, edge profile and allowable camber. Include surface quality and any intermediate annealing requirements. | Defines the input and work envelope to be included in the offer. |
| Roll stands and tension | Compare stand sequence, roll support, gap control, guides and take-up. Uneven reduction or tension can create thickness variation, edge cracks or twisting. | Determines configuration, supporting equipment and exclusions. |
| Production acceptance | Roll representative wire and inspect section dimensions, edge integrity, straightness, surface and material properties where required. Include speed changes and coil transitions. | Establishes the agreed demonstration and inspection records. |
What must be prepared for installation?
Plan payoff, lubricant and cooling systems, strip support, guarded tension spans and finished-coil removal.
Request a connection schedule, installation drawing and responsibility matrix. Check space during maintenance as well as operation, and have the receiving site confirm that supporting services can meet the stated duty.
How should production acceptance be demonstrated?
Roll representative wire and inspect section dimensions, edge integrity, straightness, surface and material properties where required. Include speed changes and coil transitions.
Witness the agreed challenge cases and keep the settings that produced them. A factory acceptance result should be repeatable after installation, with measuring instruments and site differences clearly identified.
Which service provisions protect repeatability?
Inspect roll profiles, bearings, guides, gap measurement and tension devices; preserve reduction recipes by material condition.
Ask for maintenance instructions tied to the delivered configuration. The offer should distinguish operator consumables, periodic specialist work and parts with uncertain lead times, with training covering safe fault finding and recovery.
What can be customized through OEM or ODM?
OEM gauges and take-up can be configured; ODM special profiles require roll design and formability trials.
Submit the proposed changes with the wire flattening rolling line duty and acceptance plan. Separate a purchased option from new engineering, and agree drawings, validation responsibility, documentation and spare-part support before design release. The manufacturer example is a technical reference only; customization does not imply permission to copy protected designs or use a brand.
Request an itemized offer that identifies tooling or auxiliaries, freight assumptions, commissioning, operator training and recurring consumables. Agree who supplies trial inputs and inspection instruments, and resolve deviations before comparing the complete project cost.
What should your wire flattening rolling line RFQ include?
- Wire flattening rolling line application and required process result
- Wire and final section: Provide alloy, inlet diameter, hardness, target width, thickness, edge profile and allowable camber. Include surface quality and any intermediate annealing requirements.
- Roll stands and tension: Compare stand sequence, roll support, gap control, guides and take-up. Uneven reduction or tension can create thickness variation, edge cracks or twisting.
- Representative input variation and difficult production cases
- Required acceptance evidence: Roll representative wire and inspect section dimensions, edge integrity, straightness, surface and material properties where required. Include speed changes and coil transitions.
- Site and utility scope: Plan payoff, lubricant and cooling systems, strip support, guarded tension spans and finished-coil removal.
- Service provision: Inspect roll profiles, bearings, guides, gap measurement and tension devices; preserve reduction recipes by material condition.
- OEM/ODM engineering scope: OEM gauges and take-up can be configured; ODM special profiles require roll design and formability trials.
- Upstream preparation and downstream handling interfaces
- Destination country and applicable installation requirements
- Production schedule, changeover mix and operator availability
- Drawings, samples, inspection method and rejected-output criteria
Need OEM / ODM customization?
Submit branding, packaging, configuration or engineering requirements for this equipment. Include the target market, initial and annual quantities, required changes and acceptance criteria.
Customization feasibility, permitted branding, development responsibilities, minimum quantity, cost and lead time are reviewed for the proposed supplier and configuration before a quotation is confirmed.
Frequently asked questions
What defines the application boundary for wire flattening rolling line?
A flattening line rolls round wire into a controlled flat or profiled section. Reduction schedule, edge behavior and tension control determine the final strip rather than width alone. Transforms wire into controlled flat profiles; roll setup and section tolerance define the process. Define the intended production result before comparing nominal ratings, and ask for evidence using the actual input conditions.
What should the wire flattening rolling line RFQ state about wire and final section?
Provide alloy, inlet diameter, hardness, target width, thickness, edge profile and allowable camber. Include surface quality and any intermediate annealing requirements. Send the representative inputs and the difficult cases together, then require the supplier to state any restrictions or preparation steps needed to repeat the proposed result.
How should roll stands and tension be checked?
Compare stand sequence, roll support, gap control, guides and take-up. Uneven reduction or tension can create thickness variation, edge cracks or twisting. Ask the bidder to document the selected arrangement and exclusions against the real duty. Confirm which supporting components and setup work are included in the commercial scope.
What acceptance test is appropriate for wire flattening rolling line?
Roll representative wire and inspect section dimensions, edge integrity, straightness, surface and material properties where required. Include speed changes and coil transitions. Agree the sampling method and rejection criteria before the trial, and keep configuration and inspection records for the later site-acceptance comparison.
What installation and service details should be confirmed?
Plan payoff, lubricant and cooling systems, strip support, guarded tension spans and finished-coil removal. Inspect roll profiles, bearings, guides, gap measurement and tension devices; preserve reduction recipes by material condition. Allocate local preparations and specialist support to named parties before shipment so commissioning and subsequent maintenance have a clear owner.
Can wire flattening rolling line configurations be customized through OEM or ODM?
OEM gauges and take-up can be configured; ODM special profiles require roll design and formability trials. Supply drawings and operating conditions for feasibility review. Engineering changes require agreed validation and documentation; a reference brand image does not establish an authorized supply or manufacturing relationship.
Reference information
- FUHR Multi-stand wire rolling production line official product reference
- FUHR Multi-stand wire rolling production line technical or family reference
Reference data and images explain equipment configurations. IndustryApex engineers confirm the offered model, specification and commercial scope in your project quotation.