
A hot-runner system distributes polymer melt inside injection tooling to the selected gates. Part geometry, resin, cavity layout and thermal balance require coordinated mold engineering; it is not a stand-alone guarantee of molding quality. An evenly heated manifold can still create unbalanced fill or material degradation. Trial the complete mold and document the process window. Mold production material, inspect cavity fill, dimensions, gate appearance and color changes and record stable operation across the agreed process window. OEM/ODM requests are assessed against the intended application, site interfaces and documented acceptance evidence; the reference photograph identifies a product family and does not confirm supply availability or an authorized brand relationship.
A hot-runner system distributes polymer melt inside injection tooling to the selected gates. Part geometry, resin, cavity layout and thermal balance require coordinated mold engineering; it is not a stand-alone guarantee of molding quality.
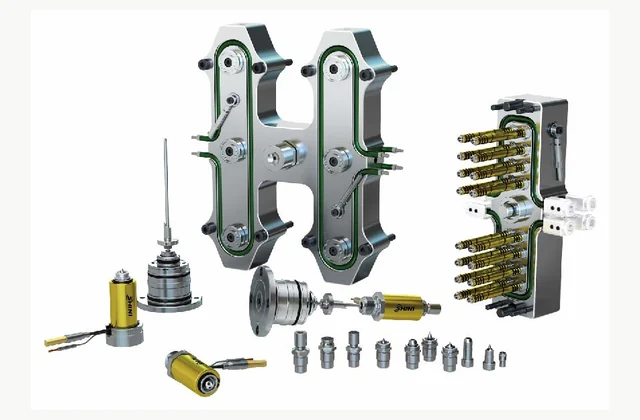
Shown as a configuration reference. Availability and the equipment offered for your project are confirmed separately.
What task does the hot runner system need to perform?
A hot-runner system distributes polymer melt inside injection tooling to the selected gates. Part geometry, resin, cavity layout and thermal balance require coordinated mold engineering; it is not a stand-alone guarantee of molding quality.
An evenly heated manifold can still create unbalanced fill or material degradation. Trial the complete mold and document the process window.
How should resin and layout be specified?
Provide polymer grade, additives, part drawings, cavities and flow-length constraints. Manifold and nozzle arrangements must fit the mold and material residence requirements.
State the required outcome and the operating cases that matter most to the project. Ask for written configuration limits and test conditions so alternative proposals can be compared without assuming that a shared product name means equivalent capability.
Which configuration choices affect gate and balance?
Compare gate type, thermal control, pressure balance and valve timing where used. Cosmetic requirements and vestige limits must be reviewed with the actual part.
| Decision | Evidence to compare | What the offer should clarify |
|---|---|---|
| Resin and layout | Provide polymer grade, additives, part drawings, cavities and flow-length constraints. Manifold and nozzle arrangements must fit the mold and material residence requirements. | Included tools, input limits and the configuration needed for the stated duty. |
| Gate and balance | Compare gate type, thermal control, pressure balance and valve timing where used. Cosmetic requirements and vestige limits must be reviewed with the actual part. | Supporting services, process interfaces and any excluded development work. |
| Application acceptance | Mold production material, inspect cavity fill, dimensions, gate appearance and color changes and record stable operation across the agreed process window. | Test method, inspection records, responsibility and treatment of deviations. |
What should be prepared before installation?
Coordinate mold pockets, wiring, controller zones, cooling separation, assembly clearances and safe maintenance access.
Resolve supporting services and access early enough to affect the design. Keep a responsibility matrix with the layout so auxiliary equipment, local preparations and commissioning checks have clear owners before shipment.
What evidence should establish application acceptance?
Mold production material, inspect cavity fill, dimensions, gate appearance and color changes and record stable operation across the agreed process window.
Retain the accepted configuration and a signed results record. If tools, inputs or controls change after the trial, review the affected evidence rather than assuming that the earlier result automatically covers the revised scope.
How should service and repeatability be planned?
Inspect heaters, thermocouples, seals, tips and valve components; retain zone maps and assembly procedures.
Review support in the destination market, including documentation language, service access and critical spare availability. Record warranty terms separately from ordinary consumables and the maintenance actions needed to preserve the accepted condition.
What can be customized through OEM or ODM?
Manifolds, nozzles, gates and controls may be engineered; new materials or cavity arrangements require molding validation.
Submit the requested changes with the hot runner system application, drawings and acceptance requirements. Distinguish standard options from new engineering and agree design ownership, validation, documentation and spare-part support before release. The illustrated manufacturer example is a technical reference; it does not establish stock, agency or permission to reproduce protected designs.
How should the quotation boundary be recorded?
Use the hot runner system inquiry to list base equipment, tooling, auxiliary services, commissioning and training separately. Record unresolved assumptions about resin and layout and gate and balance before comparing prices. Keep the final configuration and accepted evidence together so later changes can be reviewed against a clear scope.
What should your hot runner system RFQ include?
- Hot runner system application and required finished result
- Resin and layout: Provide polymer grade, additives, part drawings, cavities and flow-length constraints. Manifold and nozzle arrangements must fit the mold and material residence requirements.
- Gate and balance: Compare gate type, thermal control, pressure balance and valve timing where used. Cosmetic requirements and vestige limits must be reviewed with the actual part.
- Representative input variation and difficult operating conditions
- Application risks and exclusions: An evenly heated manifold can still create unbalanced fill or material degradation. Trial the complete mold and document the process window.
- Site and supporting services: Coordinate mold pockets, wiring, controller zones, cooling separation, assembly clearances and safe maintenance access.
- Acceptance method and retained evidence: Mold production material, inspect cavity fill, dimensions, gate appearance and color changes and record stable operation across the agreed process window.
- Maintenance and support scope: Inspect heaters, thermocouples, seals, tips and valve components; retain zone maps and assembly procedures.
- OEM/ODM changes requested: Manifolds, nozzles, gates and controls may be engineered; new materials or cavity arrangements require molding validation.
- Destination, local installation conditions and documentation language
- Drawings, samples, tooling ownership and revision control
- Operating sequence, changeovers, training and commissioning responsibilities
Need OEM / ODM customization?
Submit branding, packaging, configuration or engineering requirements for this equipment. Include the target market, initial and annual quantities, required changes and acceptance criteria.
Customization feasibility, permitted branding, development responsibilities, minimum quantity, cost and lead time are reviewed for the proposed supplier and configuration before a quotation is confirmed.
Frequently asked questions
What defines a suitable application for hot runner system?
A hot-runner system distributes polymer melt inside injection tooling to the selected gates. Part geometry, resin, cavity layout and thermal balance require coordinated mold engineering; it is not a stand-alone guarantee of molding quality. An evenly heated manifold can still create unbalanced fill or material degradation. Trial the complete mold and document the process window.
What should the buyer specify about resin and layout?
Provide polymer grade, additives, part drawings, cavities and flow-length constraints. Manifold and nozzle arrangements must fit the mold and material residence requirements. Include representative variation and ask the bidder to identify restrictions before selecting the offered configuration.
How should gate and balance be compared?
Compare gate type, thermal control, pressure balance and valve timing where used. Cosmetic requirements and vestige limits must be reviewed with the actual part. Confirm which tools, supporting services and operating conditions are included; require evidence for the actual application rather than an unloaded demonstration.
What acceptance test should be agreed for hot runner system?
Mold production material, inspect cavity fill, dimensions, gate appearance and color changes and record stable operation across the agreed process window. Agree the method, records and decision criteria before ordering, then retain the setup and results for repeatability checks after installation.
Which installation and service provisions need confirmation?
Coordinate mold pockets, wiring, controller zones, cooling separation, assembly clearances and safe maintenance access. Inspect heaters, thermocouples, seals, tips and valve components; retain zone maps and assembly procedures. Allocate local preparations and specialist service to named parties before delivery.
Can the hot runner system be customized through OEM or ODM?
Manifolds, nozzles, gates and controls may be engineered; new materials or cavity arrangements require molding validation. Submit the requested changes and drawings for feasibility review. New engineering requires agreed validation and documentation; the reference image does not establish a supply or brand relationship.
Reference information
- Shini - Hot Runner Systems For High Quality Plastic Production
- SHINI PLASTICS TECHNOLOGIES, INC.
Reference data and images explain equipment configurations. IndustryApex engineers confirm the offered model, specification and commercial scope in your project quotation.